

 Deutsch
 English
 Italiano



Process selection: which manufacturing process suits your part?
The right manufacturing process depends on the part: on the material, the required properties, the geometry, the quantity and the demands on surface and accuracy. Only the combination of these factors determines whether 3D printing, CNC machining or a casting process makes technical and economic sense.
On the PROTIQ Marketplace you will find over 12 processes – from laser sintering and laser melting of metal to injection moulding. This page helps you with the preselection. After uploading, you choose the process and material and usually see the price and production time straight away; the system automatically checks whether the part fits into the build space. If you are unsure, please get in touch.
Process selection at a glance
- Material groups
- Plastics, metal, ceramics and glass
- Offering
- over 160 materials and over 12 processes, additive and conventional
- Key criteria
- Material, requirements, geometry, quantity, surface and accuracy
- Price
- usually directly in the configurator, otherwise via price request
- Advice
- personal, from the PROTIQ team
5 questions about the process
How do I find the right manufacturing process?
Answer five questions for your part – step by step, they narrow down the processes that come into question.
- Which material?Plastics, metal, ceramics or glass? The material narrows the choice the most – not every process handles every material group.
- Which requirements?Does the part need to withstand loads, be elastic, conductive, temperature-resistant, transparent or flame-retardant? This determines material and process.
- How complex and how large is the part?Internal channels, undercuts or lattice structures point to 3D printing; simple prismatic shapes can often be milled or turned more economically. Every process has a limited build space – when you upload, the system automatically checks whether your part fits.
- What quantity?For prototypes, single parts and small batches, 3D printing is often economical because no tooling is required. For large quantities, casting processes with tooling usually pay off.
- Which surface and accuracy?Smooth visible surfaces, fine details or tight tolerances? Resin-based processes deliver smooth surfaces; for tight tolerances, CNC machining is often the better choice.
Quick selection
Which process suits which requirement?
Start with the most important requirement for your part. The quick selection shows which processes typically come into question – one click takes you to the respective process page.
Load-bearing plastic parts
Industrial functional and visible parts made of polyamide and other thermoplastics, produced in the powder bed without support structures.
Resin-based: details and high-performance resins
Resin-based processes for design models, housings and detailed prototypes; Hot Lithography with high-performance resins, for example flame-retardant or electrically insulating.
Elastic and rubber-like
Soft, flexible parts, for example made of elastomers, TPU or silicone-like materials.
Special materials and larger parts
Flame-retardant, fibre-reinforced, dissipative or conductive thermoplastics, depending on the machine also for larger parts.
Models, gauges and prototypes
Powder bed process without support structures – with PMMA-based plastics that are easy to machine.
Metal functional parts
Parts made of steel, aluminium, titanium, copper, brass or zinc alloy, among others – including internal channels.
Small, delicate metal parts
Small parts made of stainless steel with fine details and, depending on the material, a smooth surface.
Electrically and thermally conductive
Copper materials processed by laser melting, for example for inductors or heat exchangers.
Transparent, made of real glass
Parts made of fused silica, transparent and temperature-resistant.
Simple geometry, tight tolerances
Prismatic or rotationally symmetrical parts made of metal or plastic, milled or turned.
Small batches to large series
Injection moulding with tooling for plastic parts in large quantities; vacuum casting from a silicone mould for small batches.
3D printing · plastics3D printing · metal3D printing · ceramics & glassConventional
The quick selection is a guide and does not replace a case-by-case review. You can see which materials are currently available in the configurator after uploading.
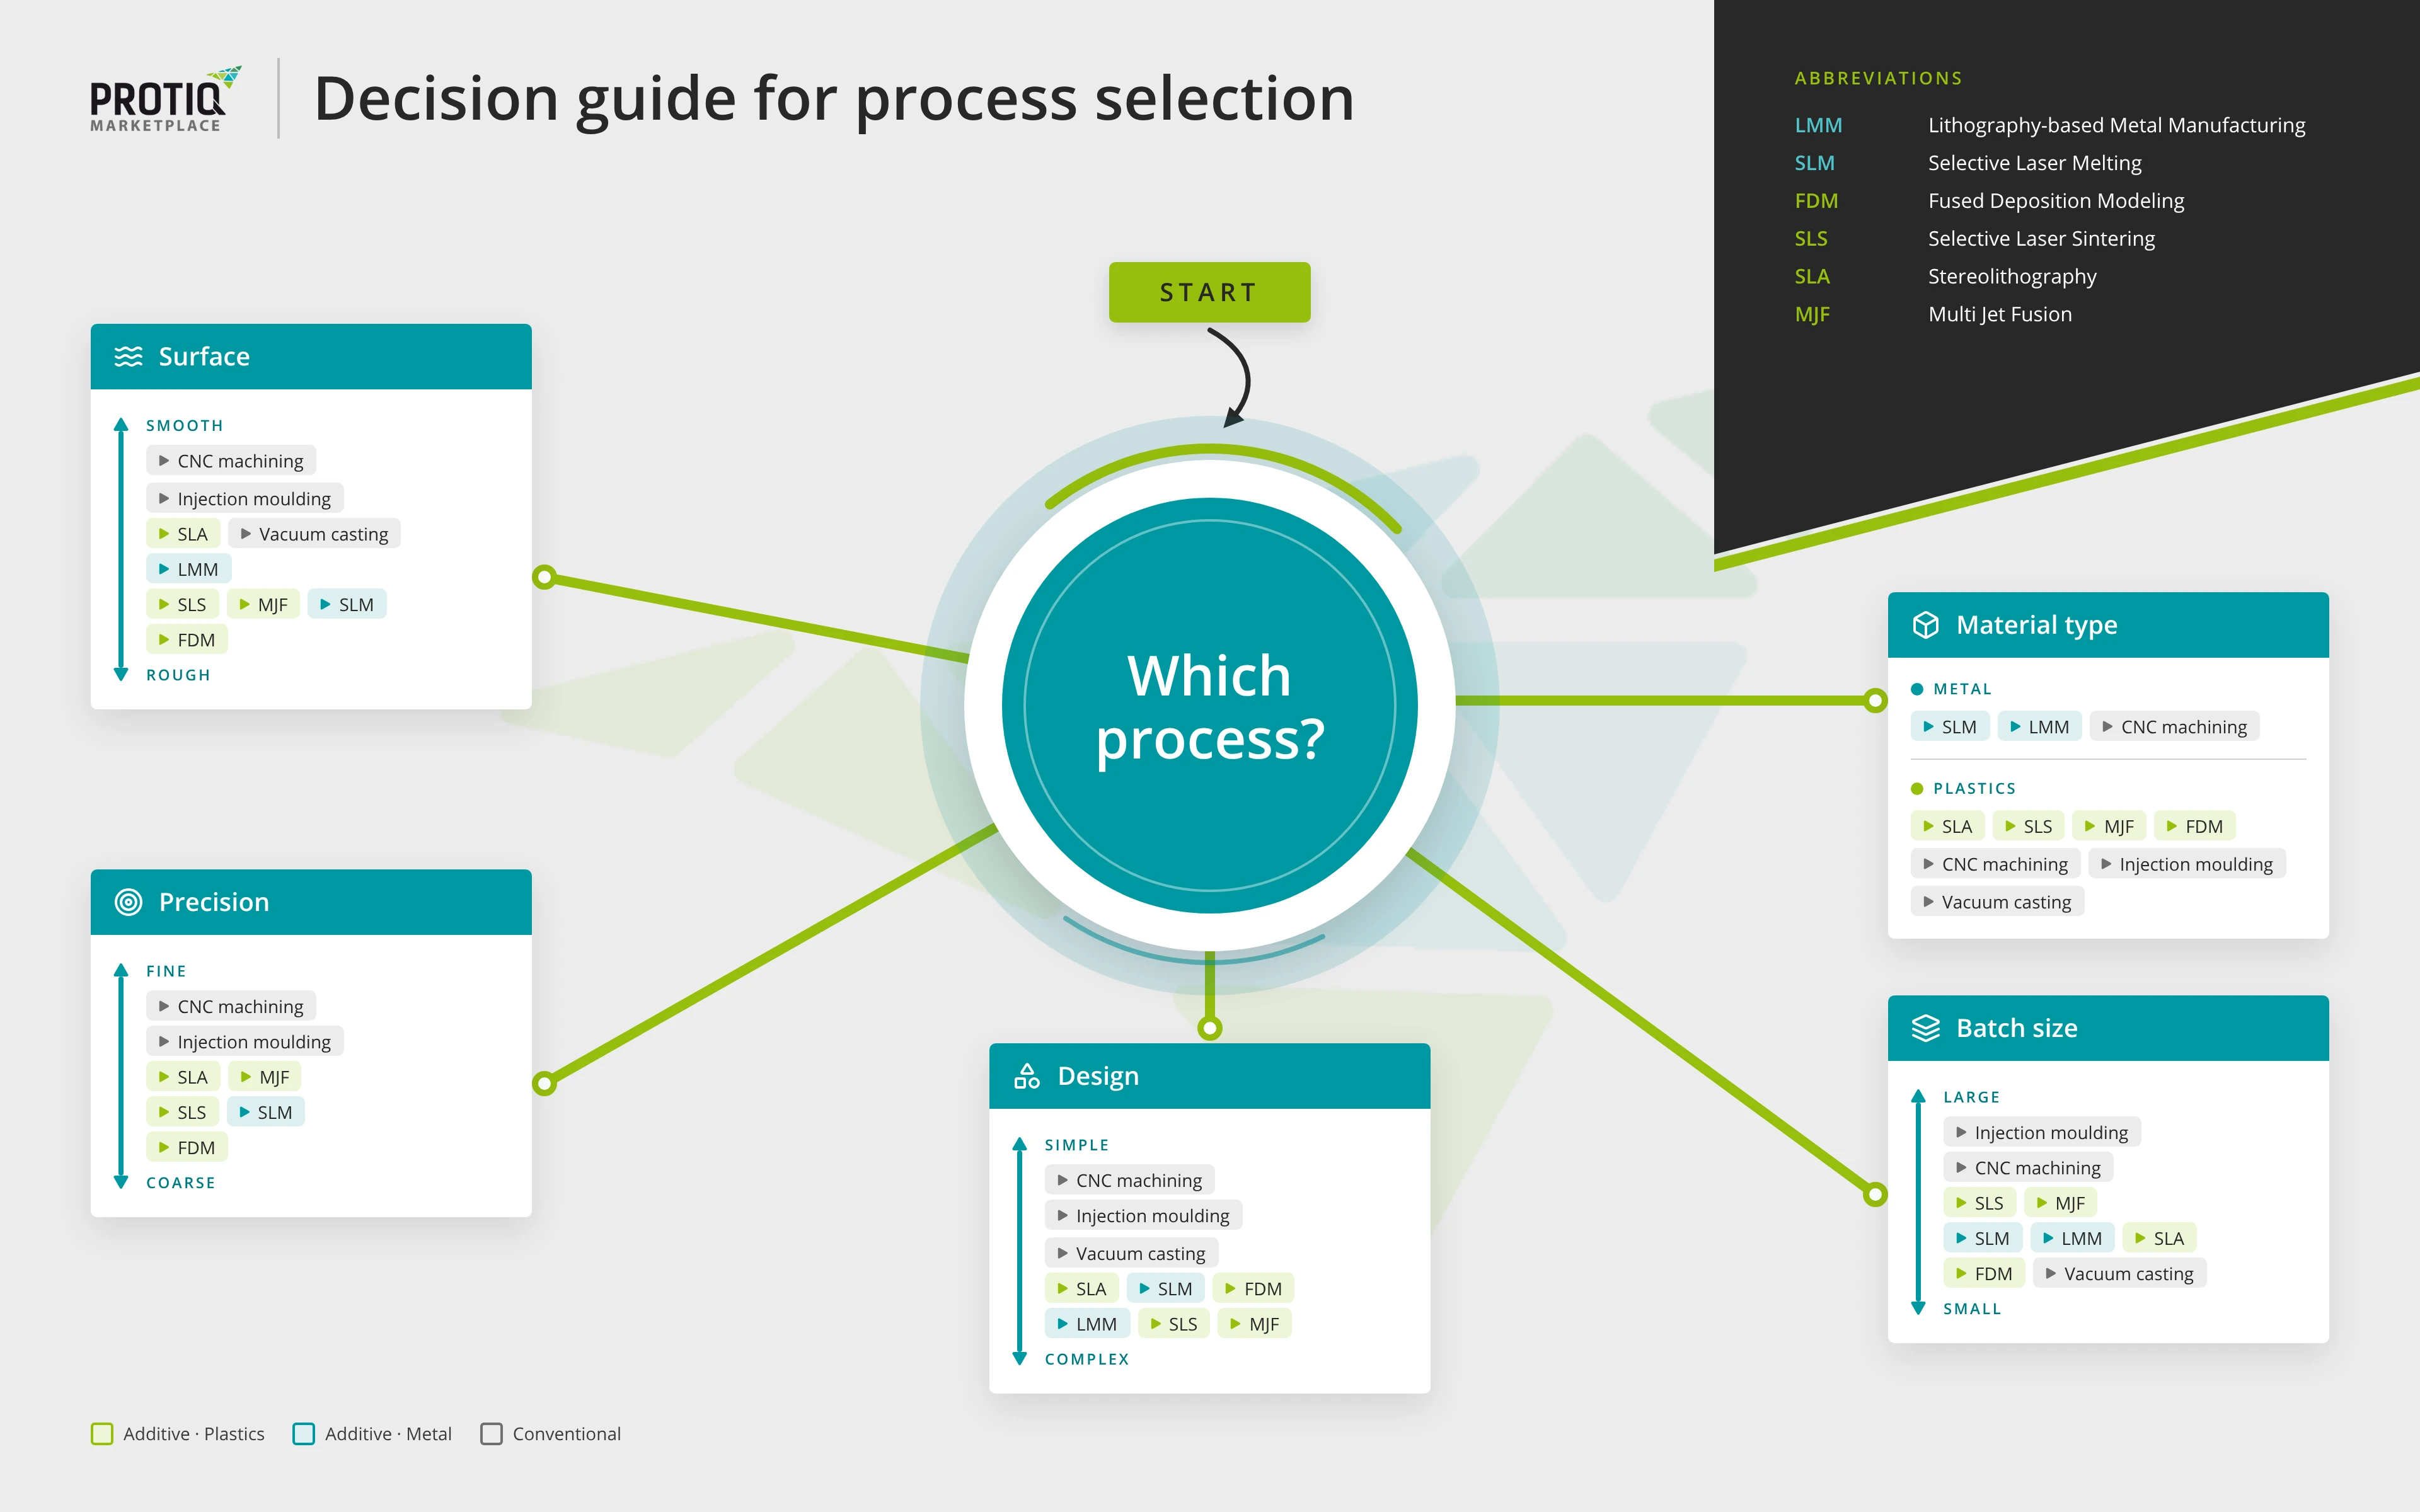
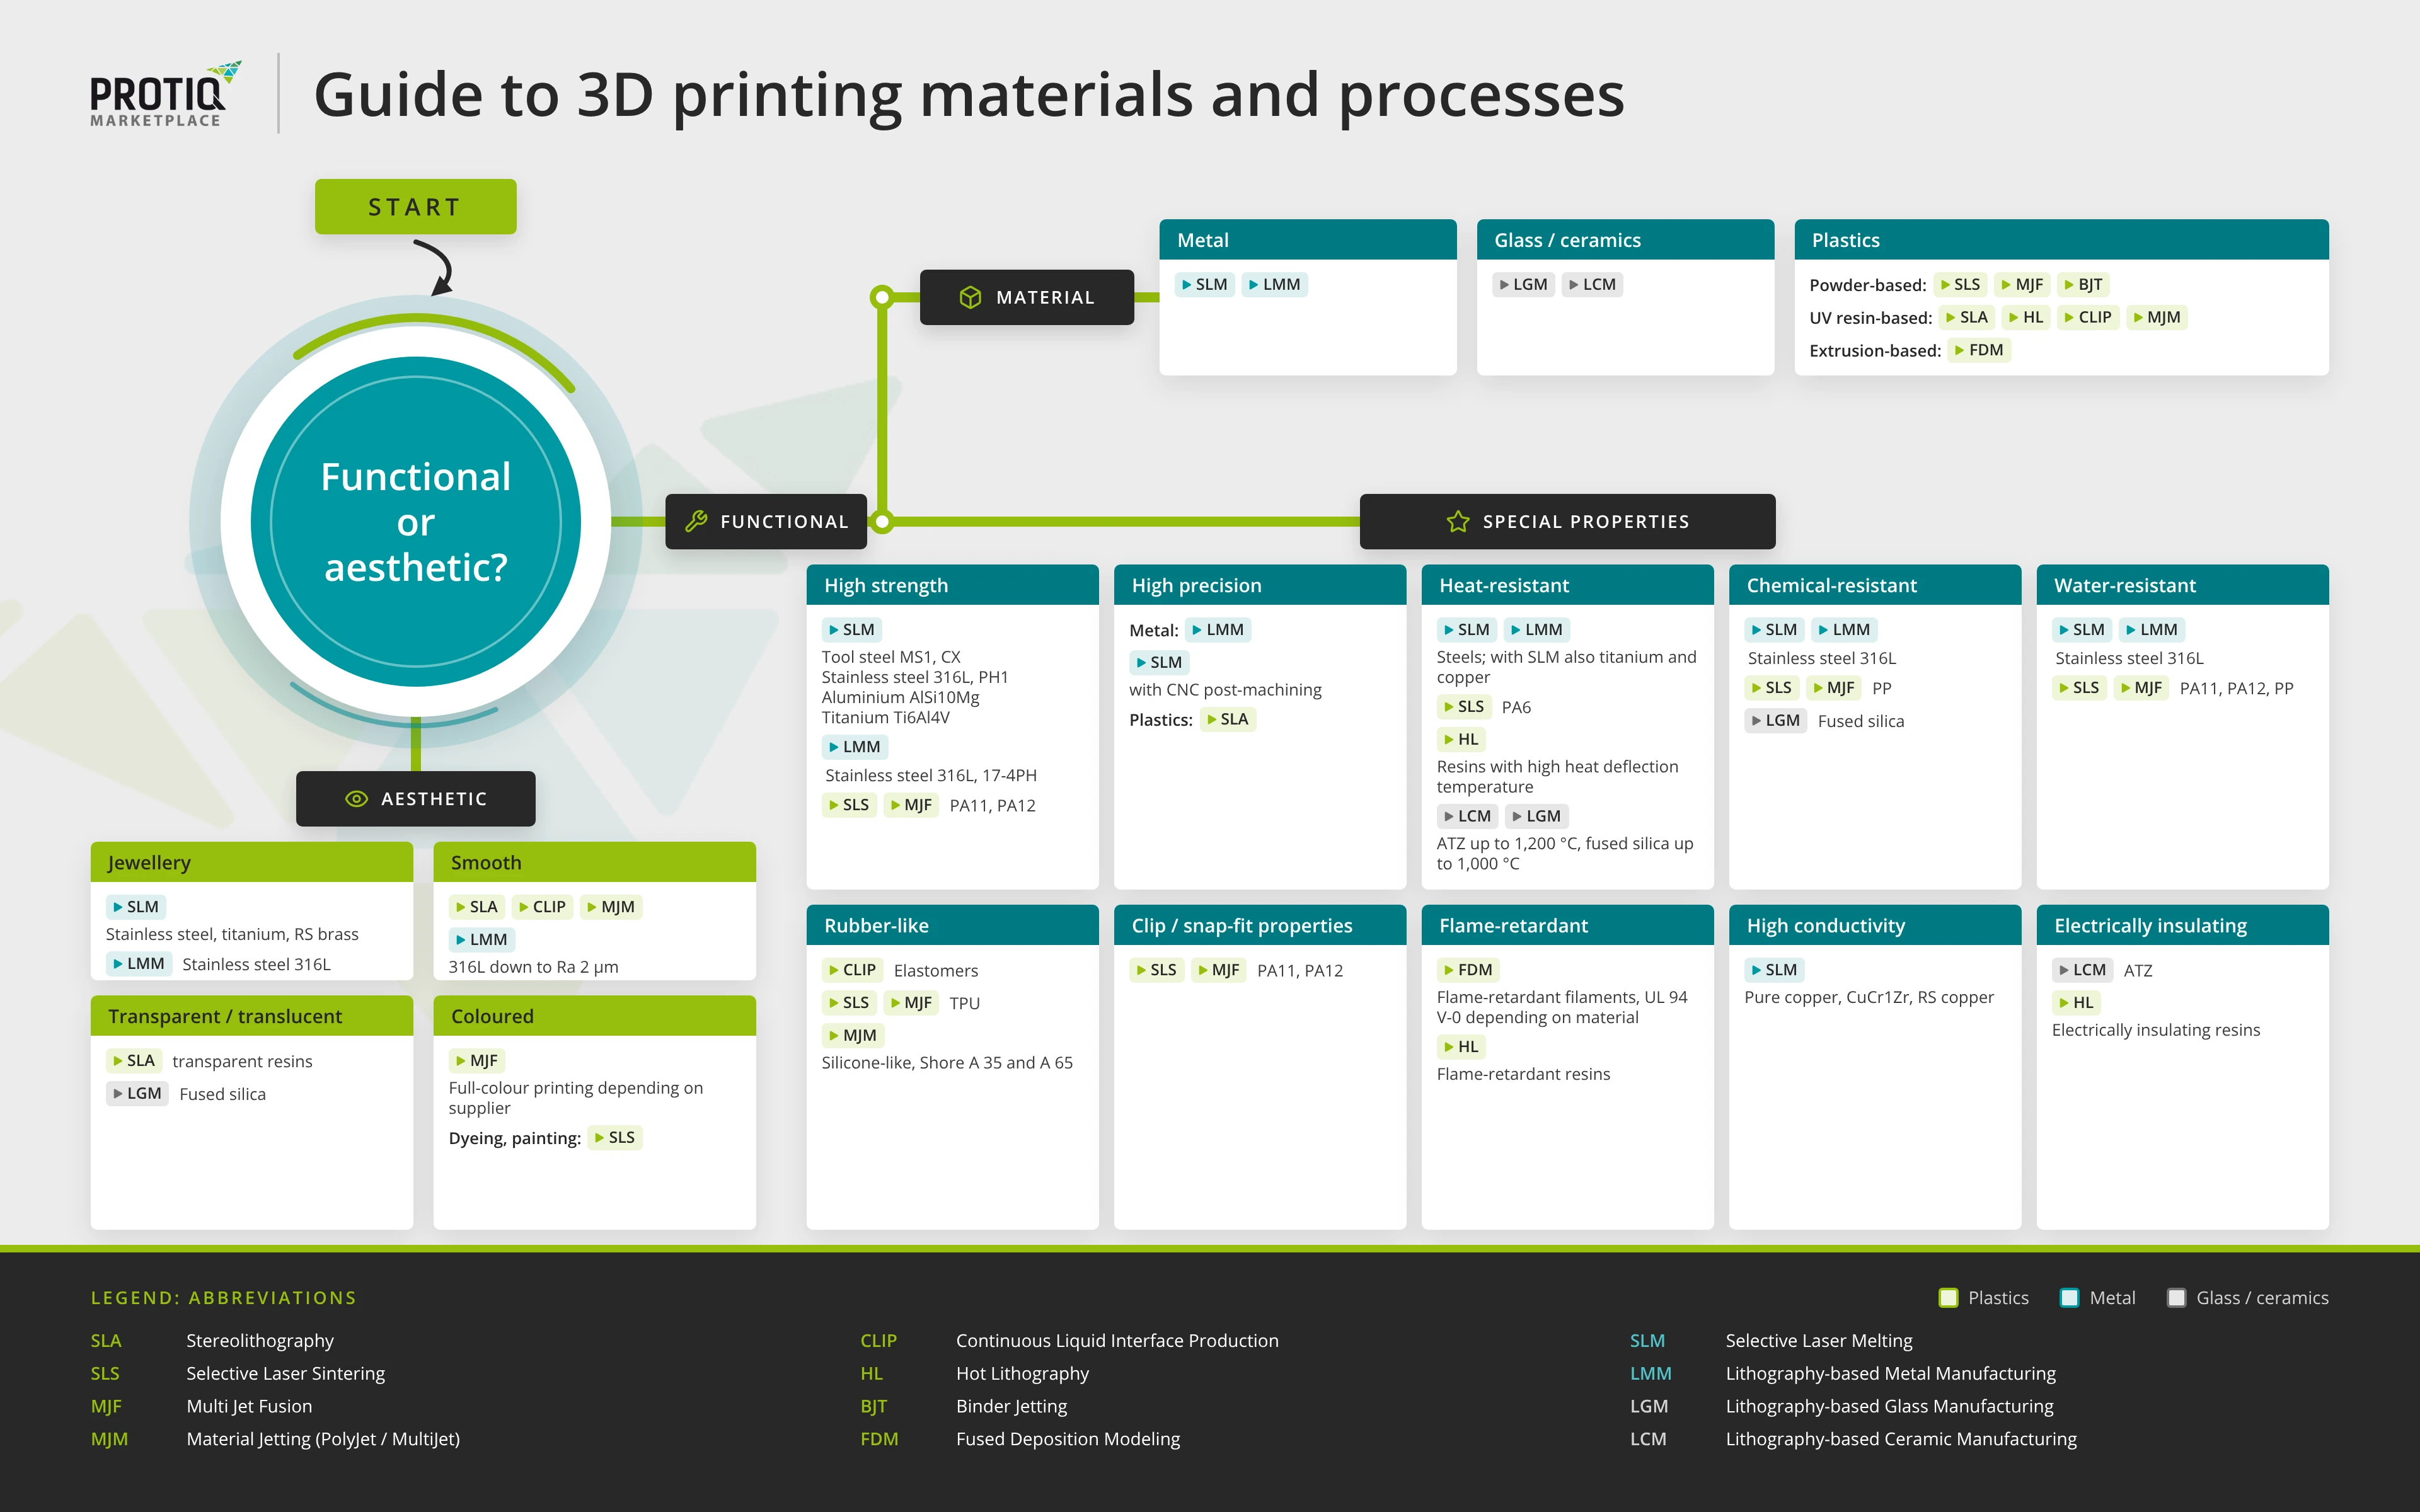
Overview graphics to enlarge
Both graphics summarise the selection at a glance and serve as a rough guide. Click on a graphic to open it in full size.
 Enlarge
 Enlarge
Processes compared
How do the 3D printing processes differ?
The 3D printing processes on the PROTIQ Marketplace differ above all in material, surface and intended use. The table summarises the most important differences; you will find details on the process pages.
| Process | Materials | Strengths | Please note |
|---|---|---|---|
| Laser sintering (SLS) | PA12, PA11, PA6, TPU, PP and others | load-bearing, no support structures, complex geometries | surface slightly rough, matt |
| Multi Jet Fusion (MJF) | PA12, PA11, PP, TPU | functional parts without support structures | greyish base colour as standard |
| Stereolithography (SLA) | synthetic resins (photopolymers) | smooth surfaces, fine details | support structures required |
| Hot Lithography (HL) | high-viscosity photopolymers | high-performance resins, walls from 0.3 mm | support structures usually required |
| CLIP / DLS | epoxy, PU and methacrylate resins, elastomers | robust and elastic parts, smooth surface | support structures required |
| Material Jetting (PolyJet / MultiJet) | currently silicone-like materials, Shore A 35 and A 65 | soft parts, 30 µm layer thickness | support material required |
| Binder Jetting (BJT) | PMMA-based plastics | no support structures, easy to machine | surface slightly rough |
| Fused Deposition Modeling (FDM) | thermoplastics, also flame-retardant, fibre-reinforced, conductive | special materials, larger parts | visible layer lines, direction-dependent properties |
| Laser melting (SLM) | steel, aluminium, titanium, copper, brass, zinc alloy and others | metal functional parts, internal channels | support structures required |
| Lithography-based Metal Manufacturing (LMM) | stainless steels, e.g. 316L and 17-4PH | small, delicate parts, smooth surface | small parts only |
| Ceramics (LCM) | technical ceramics, e.g. ATZ | hard, temperature-resistant, electrically insulating | small parts, brittle |
| Glass (LGM) | fused silica | transparent, usable up to 1,000 °C | wall thickness 0.8–5 mm, tolerances ± 250 µm (uncoated) |
Overview based on the process pages and datasheets on the PROTIQ Marketplace; no guaranteed properties. The supplier’s information in the ordering process or in the quotation is authoritative.
↑ Back to overview3D printing or conventional?
When is a conventional process the better choice?
3D printing plays to its strengths with complex geometries, prototypes and small to medium quantities because no tooling is required. Simple geometries with tight tolerances can often be milled or turned more economically, and large quantities are better suited to injection moulding.
| 3D printing | CNC machining | Injection moulding | Vacuum casting | |
|---|---|---|---|---|
| Tooling | not required | not required | mould or tool required | silicone mould from a master model |
| Typical quantity | single part to small batch, depending on the process also series | single part to medium series | large quantities | prototypes and small batches |
| Geometry | complex, including internal channels | rather simple, prismatic or rotationally symmetrical | limited by tool and demouldability | limited by mould and demouldability |
| Tolerances | process-dependent | tight tolerances possible | tight, tool-dependent | dependent on master model and casting resin |
- CNC machiningFor simple, prismatic or rotationally symmetrical parts made of metal or plastic, especially when tight tolerances are required.
- Injection mouldingThe standard for plastic parts in large quantities. The tool is an investment that is spread across the quantity.
- Vacuum castingSmall batches from a silicone mould. The master model can come from 3D printing – so printed geometries can be replicated.
- Zamak 5 in 3D printingFor zinc parts in large quantities, die casting with tooling is economical. Prototypes and small batches made of the die-casting material Zamak 5 are produced by laser melting – without a die-casting tool.
Process groups
Which groups of 3D printing processes are there?
3D printing processes can be distinguished by how the material is solidified. This results in typical strengths and limitations for each group.
Powder bed
A thin layer of powder is spread and selectively solidified – by a laser (SLS, SLM), by a printed fusing agent combined with infrared light (MJF) or by a binder (Binder Jetting). The surrounding powder supports plastic parts, whereas laser melting of metal requires support structures.
Photopolymerisation
A liquid, light-curing resin is cured with light – layer by layer (SLA, Hot Lithography) or continuously (CLIP). SLA and CLIP deliver comparatively smooth surfaces and fine details; Hot Lithography processes heated, high-viscosity high-performance resins.
Lithography with subsequent sintering
A mixture of metal, ceramic or glass particles and a light-curing binder is exposed. The green part is then debound and sintered – resulting in parts made of metal, ceramics or glass.
Multi Jet Fusion, PolyJet, MultiJet, CLIP, Digital Light Synthesis and Hot Lithography as well as other names mentioned are trademarks or designations of their respective owners. They are mentioned solely to describe the processes.
↑ Back to overviewFAQ
Frequently asked questions about process selection
How do I find the right manufacturing process for my part?
First clarify the material and requirements, then geometry, quantity, surface and accuracy. The quick selection on this page shows suitable processes for typical requirements. After uploading your file, you choose the process and material in the configurator and usually see the price and production time straight away.
Is the PROTIQ Marketplace only about 3D printing?
No. In addition to numerous 3D printing processes, you will also find CNC machining, injection moulding and vacuum casting as well as various finishing options.
When is 3D printing cheaper than conventional manufacturing?
Often for prototypes, spare parts, customised parts and small quantities, because no tools or moulds are required. For large quantities, injection moulding or die casting are usually more economical despite the tooling costs.
When do I choose 3D printing instead of CNC milling?
3D printing makes sense for complex geometries, internal channels, function integration or individual adaptations. CNC machining plays to its strengths with simple geometries and tight tolerances.
What is the difference between SLS and MJF?
Both processes produce plastic parts in the powder bed without support structures. In laser sintering, a laser melts the powder; in Multi Jet Fusion, a printed fusing agent combined with infrared light does so. MJF parts are greyish as standard.
Which 3D printing processes are available for metal?
On the PROTIQ Marketplace, selective laser melting (SLM) is the obvious choice for metal functional parts. Lithography-based Metal Manufacturing (LMM) is suitable for small, delicate parts made of stainless steel.
Why do prices differ between processes?
The price depends on the process, material, part volume, geometry, quantity and finishing, among other things. That is why the same part can cost different amounts depending on the process. In the configurator, you can compare the available offers directly.